Adresse
304 North Cardinal
St. Dorchester Center, MA 02124
Heures de travail
Du lundi au vendredi : de 7h00 à 19h00
Le week-end : 10H00 - 17H00
Adresse
304 North Cardinal
St. Dorchester Center, MA 02124
Heures de travail
Du lundi au vendredi : de 7h00 à 19h00
Le week-end : 10H00 - 17H00
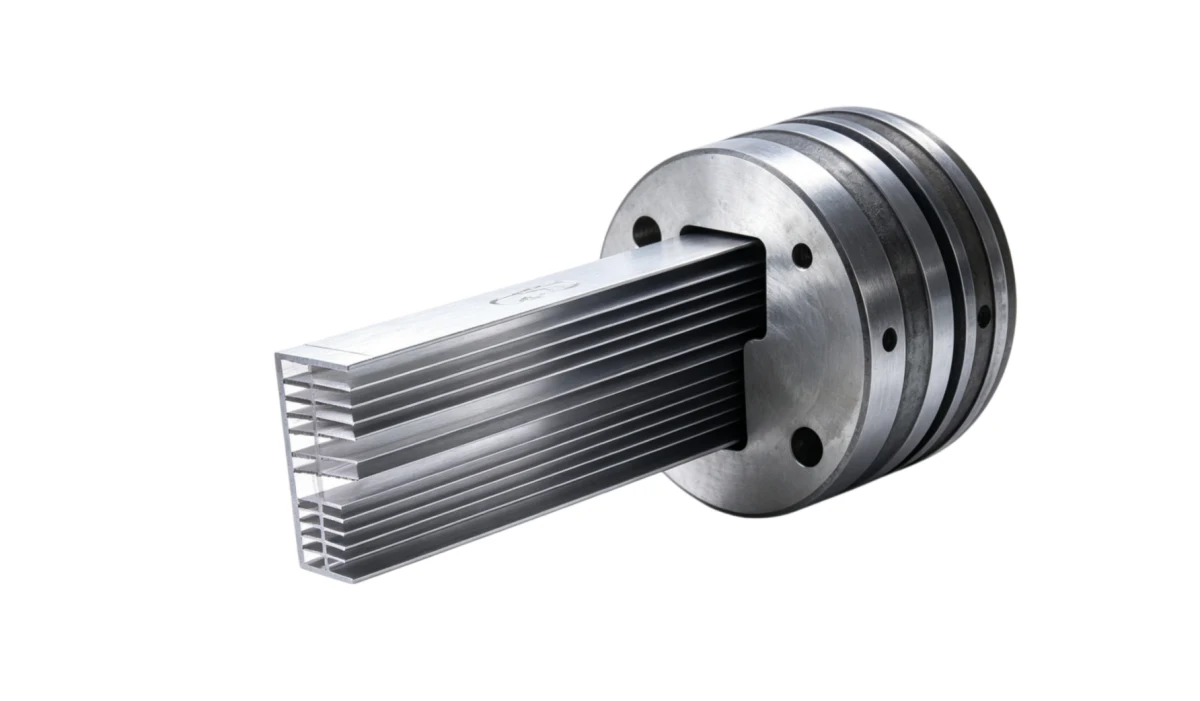
The modern aluminum manufacturing industry relies heavily on precision engineering to transform raw alloy billets into complex structural profiles. At the heart of this transformative process is the extrusion die—a specialized, heavy-duty steel tool engineered to withstand extreme pressures and thermal loads. Understanding how custom aluminum extrusion dies work is essential for B2B procurement managers, structural engineers, and product designers seeking to optimize manufacturing efficiency, reduce tooling costs, and ensure consistent dimensional accuracy.
Custom tooling provides the unique capability to produce tailored cross-sections ranging from lightweight architectural window frames to intricate micro-channel heat sinks. This comprehensive guide details the mechanics, structural classifications, precision manufacturing steps, and critical engineering parameters that govern custom aluminum extrusion die functionality.
At its most fundamental level, an aluminum extrusion die is a precision-machined steel disc containing one or more shaped openings. During the hot extrusion process, a preheated aluminum billet—typically warmed to a plastic state between $400^\circ\text{C}$ and $500^\circ\text{C}$—is pushed through the die opening by a hydraulic ram exerting thousands of tons of force. The die acts as a high-pressure mold, forcing the softened metal to flow through its shaped orifices and take on the exact cross-sectional geometry of the aperture.
+-----------------------------------------------------------------------+
|                 EXTRUSION DIE MECHANICAL FLOW SYSTEM                  |
+-----------------------------------------------------------------------+
  [1. Heated Aluminum Billet] ──> Plastic State (400°C - 500°C)
            │
            ▼
  [2. Hydraulic Ram Pressure] ──> Exerts High Tonnage Force
            │
            ▼
  [3. Die Opening & Bearing Area] ──> Regulates Flow Rate & Profile Shape
            │
            ▼
  [4. Continuous Extruded Profile] ──> Emerges onto Run-out Table
To fully grasp how custom aluminum extrusion dies work, engineers must examine the internal friction and metal flow dynamics within the tool. Analyzing how custom aluminum extrusion dies work under high tonnage pressure ensures optimal profile shape consistency and reduces extrusion defects.
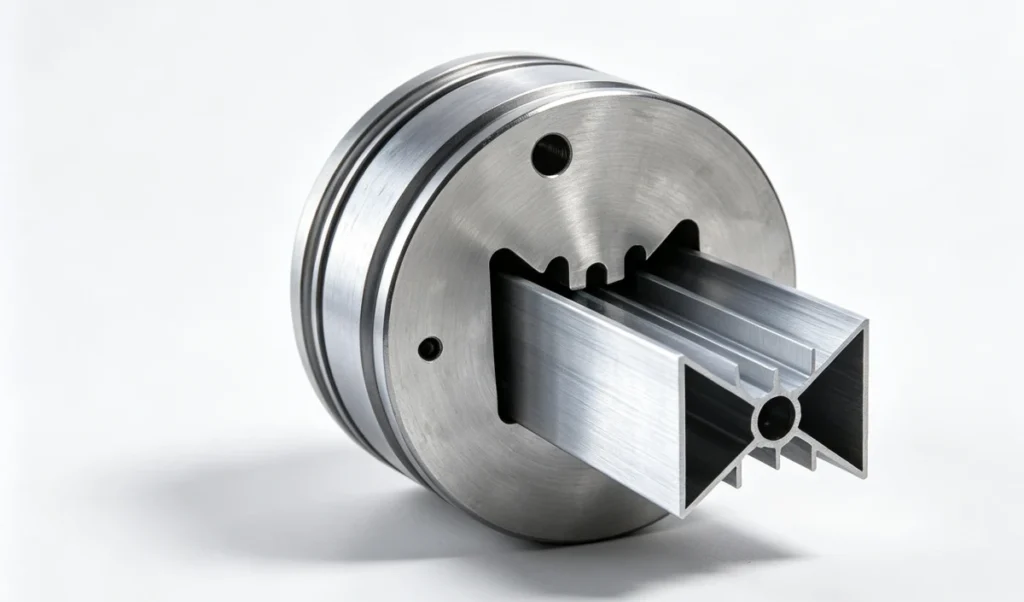
To accommodate diverse product designs, toolmakers utilize two primary architectural categories of extrusion dies: solid dies and hollow (or porthole) dies. Tooling architecture determines how custom aluminum extrusion dies work to form solid bars versus complex hollow tubes. Understanding how custom aluminum extrusion dies work across different solid and hollow die configurations helps buyers select the right tooling design.
Solid dies are manufactured from a single steel disc and are designed to produce solid or semi-hollow shapes, such as angle bars, channels, flat strips, and T-slot rails. The aluminum passes directly through the cut-out opening in a continuous stream. Because there are no internal cores or obstructions, solid dies are straightforward to manufacture, cost-effective, and experience lower mechanical stress during operation.
Creating hollow profiles—such as square tubing, round pipes, or multi-cavity heat sinks—requires a multi-piece die assembly consisting of a mandrel plate (bridge) and a cap die.
| Feature / Parameter | Solid Extrusion Die | Hollow (Porthole) Extrusion Die |
| Tooling Components | Single steel plate | Multi-piece (Mandrel + Die Cap) |
| Profile Compatibility | Angles, Channels, Flat Bars | Tubes, Hollow Box Sections, Enclosures |
| Internal Metal Flow | Single continuous stream | Split into streams, then re-welded |
| Tooling Complexity | Modéré | Haut |
| Manufacturing Cost | Lower initial cost | Higher initial cost |
| Maintenance Level | Low to Moderate | High (Requires precise alignment) |
Evaluating how custom aluminum extrusion dies work for multi-cavity hollow profiles requires close inspection of the internal welding chamber design.
When analyzing how custom aluminum extrusion dies work for hollow shapes, the metal flow follows a unique pathway:
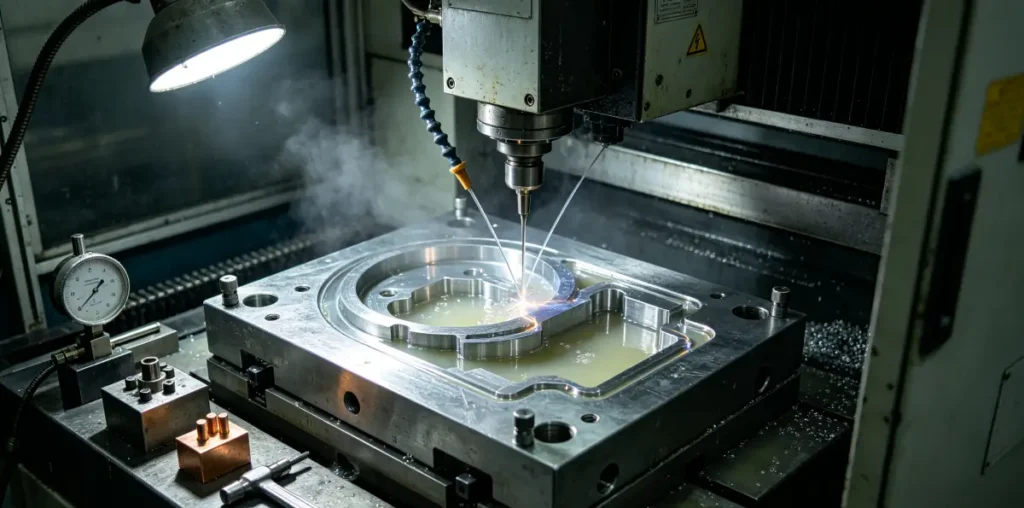
Manufacturing a custom die demands extreme metallurgical precision. Because aluminum extrusion dies operate under harsh thermal-mechanical cycles, toolmakers use high-grade hot-work tool steels, primarily AISI H13, known for exceptional toughness, red hardness, and wear resistance.
+-----------------------------------------------------------------------+
|               CUSTOM EXTRUSION DIE MANUFACTURING FLOW                 |
+-----------------------------------------------------------------------+
  [1. CAD/CAM Modeling & Simulation] ──> FEA Metal Flow Analysis
            │
            ▼
  [2. CNC Machining & Turning] ──> Rough Shaping of H13 Steel Blank
            │
            ▼
  [3. Vacuum Heat Treatment] ──> Hardened to 46-52 HRC
            │
            ▼
  [4. Wire EDM & Sinker EDM] ──> Precision Cutting of Bearing Surfaces
            │
            ▼
  [5. Polishing & Nitriding] ──> Hard Surface Coating Layer
The process begins with 3D CAD modeling. Engineers input profile dimensions into simulation software to perform Finite Element Analysis (FEA). FEA simulation reveals how custom aluminum extrusion dies work under simulated pressure, predicting metal velocity distribution. Knowing how custom aluminum extrusion dies work during CAD modeling prevents costly tooling adjustments later.
High-grade H13 steel forged discs are turned on CNC lathes to establish outer diameters and face alignments. Entry ports, feeder channels, and relief pockets are milled out. The pre-machined steel disc undergoes vacuum heat treatment (hardening and double tempering) to achieve a working hardness between $46$ and $52\text{ HRC}$.
Standard mechanical drills cannot cost-effectively machine hardened H13 steel with tight tolerances. Toolmakers employ advanced Electrical Discharge Machining:
The bearing area—the internal surface of the die aperture that directly contacts the extruding aluminum—is hand-polished to a mirror finish. Finally, the die undergoes gas nitriding, a thermochemical process that diffuses nitrogen into the steel surface, creating an ultra-hard ceramic-like iron nitride layer ($>1000\text{ HV}$) that dramatically extends die operational lifespan.
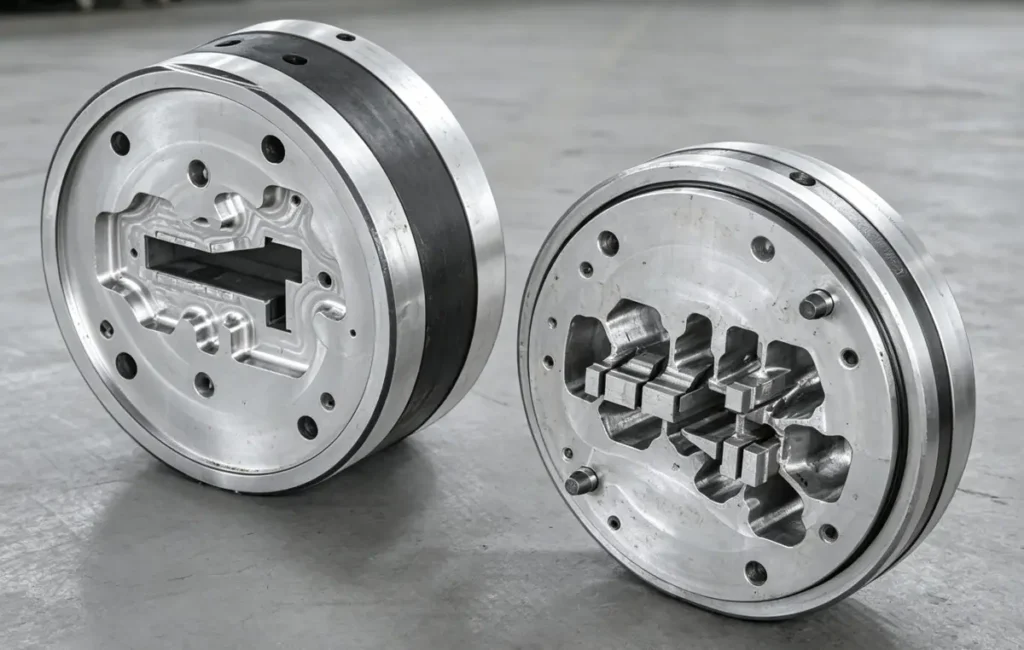
The operational success of a custom tool depends heavily on fine-tuning its critical geometric parameters.Mastering how custom aluminum extrusion dies work from a tooling design perspective helps engineers prevent profile defects. A deep technical understanding of how custom aluminum extrusion dies work allows manufacturers to optimize bearing lengths and wall thickness transitions.
The bearing surface is the section of the die opening that runs parallel to the direction of extrusion. Because aluminum flows faster through thick open areas than through thin restricted slots, tool Designers adjust the bearing lengths across different parts of the die aperture:
By fine-tuning these bearing lengths down to fractions of a millimeter, the extruded profile exits the die head evenly across its entire cross-section.
Abrupt transitions from thick to thin walls create severe thermal and velocity gradients. Aluminum cools unevenly upon exiting the die, leading to warping or residual stress concentration. Engineers recommend designing smooth radius transitions between varying wall sections to ensure uniform alloy delivery.
In shapes featuring deep channels or slots, the steel die section protruding into the metal flow is known as the “tongue.” If a slot is too deep relative to its width (a high tongue ratio), the immense hydraulic pressure of extruding aluminum can bend or break the steel tongue. Keeping tongue ratios within safe limits (typically below $3:1$ for standard profiles) ensures long tool life and structural safety.
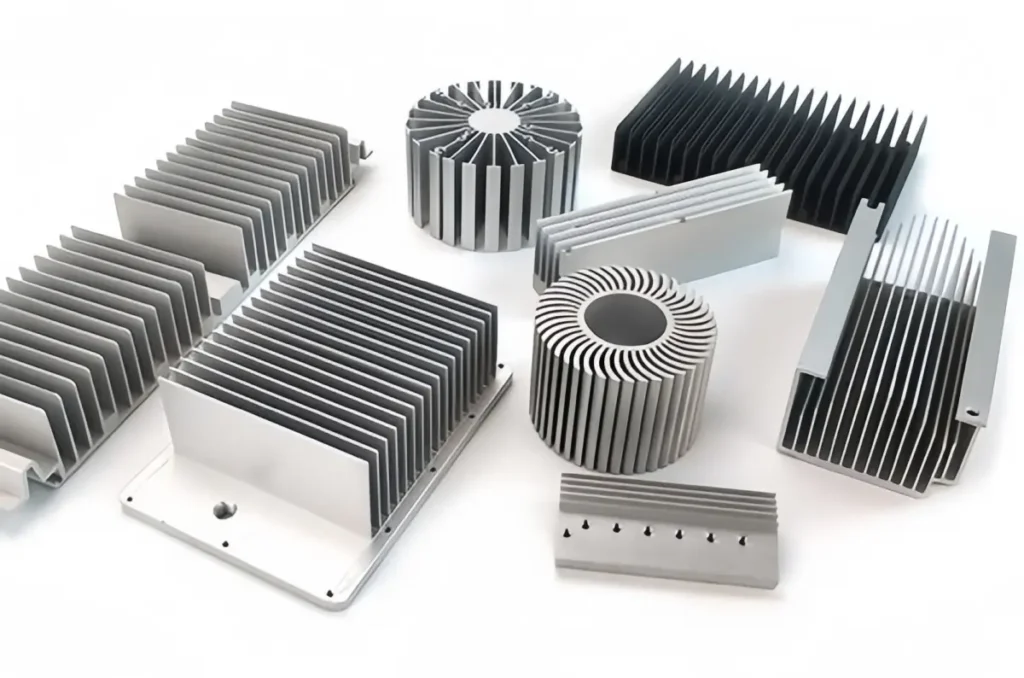
To assist engineering and procurement teams in evaluating tool feasibility and ordering custom extrusions, the following technical summary outlines industry-standard tolerances, material specs, and performance benchmarks associated with extrusion die tooling.
By mastering how custom aluminum extrusion dies work—from steel selection and EDM machining to bearing length calibration—manufacturers achieve flawless surface finishes. Contact our engineering team today to learn more about how custom aluminum extrusion dies work for your specific aluminum extrusion project.